

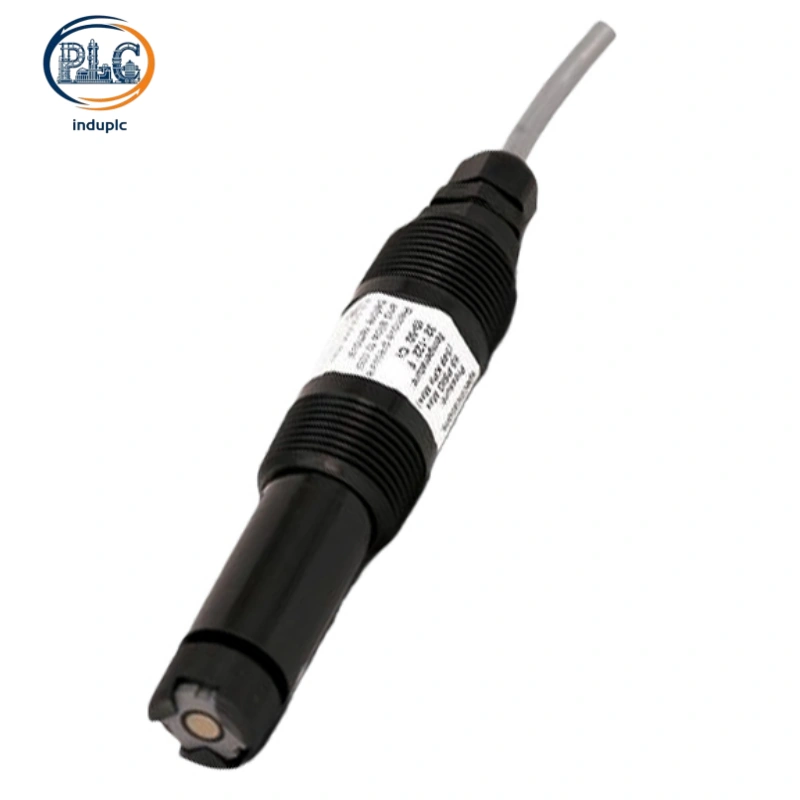
Rosemount 499ATRDO‑01 Trace Dissolved Oxygen Sensor, 0.1ppb–20ppm Ultra-High Precision Inline DO Probe for Boiler Feedwater and Condensate Monitoring
Product Description
Rosemount 499ATRDO‑01 Trace Dissolved Oxygen Sensor, 0.1ppb–20ppm Ultra-High Precision Inline DO Probe for Boiler Feedwater and Condensate Monitoring
Rosemount 499ATRDO‑01 Ultra-Low Level Trace Dissolved Oxygen Sensor for High-Purity Water Process Analysis
Precision Performance and Trace Oxygen Detection Capability
Industry-Leading Low-Level Measurement Accuracy
Rosemount 499ATRDO‑01 specializes in trace dissolved oxygen detection, covering a full measurement range from 0.1 ppb to 20 ppm. The sensor delivers exceptional low-concentration precision, achieving ±1 ppb accuracy for readings below 20 ppb and ±5% reading accuracy for concentrations above 20 ppb. Strict factory calibration eliminates baseline offset, ensuring reliable detection of micro oxygen contamination in high-purity water systems.
Stable Long-Term Drift Control
Optimized electrochemical cell design restricts signal deviation over continuous operation. Rosemount 499ATRDO‑01 maintains drift performance below 4% across 60 days of runtime, preserving consistent measurement fidelity between scheduled calibrations. Fast response time reaches 90% stable output within 20 seconds at standard ambient conditions, supporting timely process variable tracking.
Model Code Breakdown for Rosemount 499ATRDO‑01
Factory Suffix Configuration Definition
Each segment of Rosemount 499ATRDO‑01 corresponds to fixed factory specifications tailored for trace oxygen process demands. All structural and functional parameters remain preset, requiring no field modification for standard deployment.
-
499ATRDO: Premium trace dissolved oxygen sensor platform built for ultra-low ppb-level water analysis
-
‑01: Standard base configuration with integral cable assembly, optimized for general industrial high-purity water installation
This base variant prioritizes universal field adaptability, fitting most boiler and ultrapure water monitoring layouts without specialized auxiliary hardware.
Physical Specifications and Process Operating Tolerance
Temperature and Pressure Compatibility
Rosemount 499ATRDO‑01 operates steadily within 0 °C to 50 °C process temperature range, matching typical circulating water and condensate loop conditions. Process pressure tolerance spans 0 to 65 psig, accommodating standard inline pipeline pressure levels for power plant auxiliary systems and manufacturing water loops.
Durable Wet Material and Structural Design
Wetted component materials resist oxidation and water-born particle adhesion, extending operational lifespan in clean water environments. Tool-free membrane replacement simplifies on-site maintenance, reducing service downtime and eliminating reliance on specialized repair equipment. Standard 1-inch MNPT process threads enable secure inline mounting on industrial piping and sampling assemblies.
System Compatibility and Field Integration Benefits
Transmitter Pairing and Signal Adaptation
Rosemount 499ATRDO‑01 integrates seamlessly with Rosemount 1056 liquid analytical transmitters. The matched assembly converts trace oxygen readings into scalable process values, supporting local display, data logging and HART communication for DCS and PLC system acquisition. Unified instrument architecture standardizes plant analytical loop configurations.
Flexible Cable and Layout Adaptability
Standard 7.6-meter integral cable supports most conventional installation distances, with extended cable options up to 91 meters available for complex plant layouts. Flexible wiring design simplifies remote sampling point arrangement while preserving signal integrity over long transmission distances.
Core Selection Reasons and Target Industrial Applications
Key Advantages for Process Deployment
Rosemount 499ATRDO‑01 addresses critical gaps in standard DO sensor performance by capturing ppb-level oxygen contamination that impacts boiler corrosion and equipment lifespan. Low long-term drift reduces calibration frequency, while tool-free membrane maintenance cuts routine operational workload. Proven Emerson sensing technology delivers consistent performance for 24/7 continuous process monitoring.
Primary Industrial Use Cases
The sensor serves power generation boiler feedwater monitoring, steam condensate loop analysis, pharmaceutical ultrapure water quality verification and semiconductor process water control. It protects high-value process equipment from oxidation damage and maintains compliance with strict high-purity water operational standards.